In brief
- Electrically conductive materials only — and penetration is shallow
- Very shallow in steel, because ferromagnetism collapses the skin depth
- Excellent for heat exchanger tubing in non-ferrous alloys
- No couplant, no contact needed — works through thin non-conductive coatings
- We do not offer this method. Alternatives below
Eddy current testing (ECT) induces circulating electrical currents in a conductive material and detects discontinuities by the way they disturb those currents. It requires no couplant, no physical contact and no ionising radiation, and it is fast — which makes it the standard method for high-volume tube inspection and for surface crack detection in non-ferrous components.
We do not currently offer eddy current testing. This article is published as reference material. Where ECT would normally be applied, the alternatives we do provide are indicated throughout.
How it works
A coil carrying alternating current generates an alternating magnetic field. Held near a conductive material, that field induces circulating currents — eddy currents — flowing in closed loops parallel to the coil windings.
Those currents generate their own opposing magnetic field, which alters the impedance of the coil. Anything changing the flow of the eddy currents changes the coil impedance measurably: a crack interrupting their path, a change in conductivity, a change in thickness, a change in distance between probe and surface.
The instrument displays this as movement on the impedance plane — a two-dimensional plot of resistive against inductive components. Different conditions produce differently shaped and differently oriented signals, and reading those shapes is the skill of the method. A crack, a support plate and a dent each trace a characteristic pattern.
Skin effect — the property that governs everything
Eddy currents do not penetrate uniformly. Density is highest at the surface and falls exponentially with depth.
The standard depth of penetration (δ), at which current density has fallen to about 37% of its surface value, is:
δ = 1 / √(π · f · μ · σ)
where f = frequency, μ = magnetic permeability, σ = electrical conductivity
Three consequences follow directly, and they define what ECT can and cannot do:
Lower frequency penetrates deeper, at the cost of sensitivity to small defects. Frequency selection is the primary trade-off in every ECT setup.
Higher conductivity means shallower penetration. Copper and aluminium, being highly conductive, limit depth more than a poorer conductor of the same permeability.
Ferromagnetic material collapses penetration. The relative permeability of carbon steel is in the hundreds, and it sits inside the square root — so δ becomes very small indeed. Conventional ECT is effectively a surface-only method on carbon and low-alloy steel.
That last point explains why ECT dominates in heat exchangers with non-ferrous tubing and is largely absent from carbon steel structural work, where magnetic particle testing does the same job better and cheaper.
Probe types
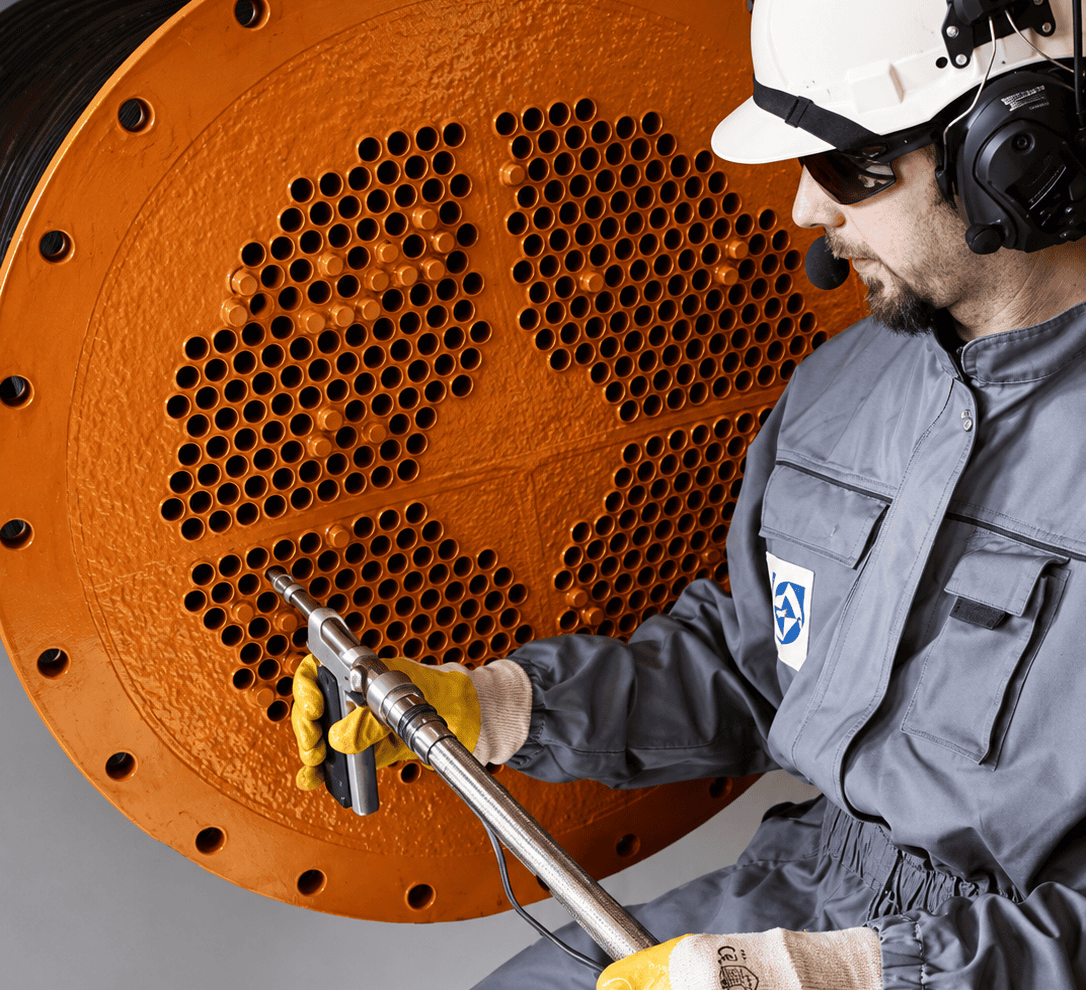
Bobbin probes — circular coils passed down the inside of a tube. Extremely fast, the workhorse of heat exchanger inspection. Weak on circumferential defects and on anything close to support plates or the tubesheet, where structural signals overwhelm the display.
Rotating probes (RFEC / motorised) — a small coil rotated as it traverses, producing a helical scan. Far better at circumferential cracking and at sizing, and much slower.
Array probes (ECA) — many elements electronically multiplexed, covering a swathe in one pass with encoded position data and C-scan imaging. The modern equivalent of moving from conventional UT to phased array.
Pencil and surface probes — small coils for spot inspection of surface cracks, common in aerospace.
Conventional ECT is often confused with its relatives, which exist precisely because of the ferromagnetic limitation:
- RFT (remote field testing) — for ferromagnetic tubing, using a through-transmission arrangement that overcomes skin depth
- NFT (near field testing) — for internal surface condition in ferromagnetic tubing, typically finned air coolers
- MFL (magnetic flux leakage) — for ferromagnetic tubing and tank floors, sensing flux escaping at wall loss
- IRIS (internal rotary inspection system) — an ultrasonic technique giving quantitative wall thickness in tubing, and generally the more reliable choice for general corrosion
Typical applications — and what we offer instead
| Application | Why ECT is used | What we provide instead |
|---|
| Heat exchanger tubing (non-ferrous) | Fast screening of thousands of tubes | Ultrasonic testing and PAUT for accessible geometry |
| Surface cracks in ferromagnetic steel | Fast, no consumables | Magnetic particle testing — higher sensitivity, established acceptance criteria |
| Surface cracks in aluminium, austenitic steel, titanium | No couplant, no contact | Penetrant testing |
| Weld inspection through thin coatings | No coating removal | PAUT or radiography |
| Wall loss and corrosion | Screening | Corrosion mapping and UTT — quantitative rather than comparative |
| Alloy sorting by conductivity | Rapid separation | PMI — identifies the actual grade, not a proxy |
Limitations
Conductive materials only. ECT requires electrical conductivity to induce currents. It cannot be used on plastics, ceramics or non-conductive composites — a point worth stating plainly, because glass and carbon-reinforced polymers are frequently and wrongly described as ECT-inspectable. Carbon fibre has limited, anisotropic conductivity, and inspecting it is a specialised research application, not routine practice.
Shallow penetration, severely so in ferromagnetic material.
Orientation matters. A discontinuity must interrupt the eddy current path to be detected. Defects parallel to the current flow produce little or no signal — the same orientation dependence that governs magnetic particle testing.
Lift-off. Distance between probe and surface strongly affects the signal. ECT does work through thin non-conductive coatings, but coating thickness is a variable that must be accounted for in calibration — not something the method handles “freely”. Beyond a certain thickness, sensitivity falls to the point where the inspection has no value.
Edge effects. Signals distort near edges, holes, welds and geometry changes, creating regions where indications cannot be resolved.
Calibration on reference standards with known artificial defects is mandatory, and the reference must match the material and geometry under test.
Interpretation is demanding. Impedance plane signals from real components include contributions from geometry, permeability variation, residual stress and surface condition alongside genuine defects. Separating them is experience, not instrumentation.
Coating thickness measurement is a different service. Instruments using eddy current or magnetic induction principles measure coating thickness under ISO 2360 and ISO 2808. That is a distinct application from flaw detection and should not be conflated with it.
Standards
| Scope | Standard |
|---|
| General principles | ISO 15549 |
| Equipment — instruments | ISO 15548-1 |
| Equipment — probes | ISO 15548-2 |
| Equipment — combined systems | ISO 15548-3 |
| Terminology | ISO 12718 |
| Steel tubes — automated ECT | ISO 10893-2 |
| US practice — non-ferrous tubing | ASTM E243 |
| US practice — general electromagnetic | ASTM E426 |
| Personnel certification | ISO 9712 |
ET is a certified method under ISO 9712. Evaluation against acceptance criteria requires Level 2 as a minimum.
Frequently asked questions
Can eddy current testing be used on carbon steel?
Only for surface-breaking defects, and with very limited depth, because ferromagnetic permeability collapses the standard depth of penetration. For surface cracks in steel, magnetic particle testing is generally more sensitive and better established.
Can eddy current testing inspect composites?
Generally no. Most composites are electrically non-conductive, so no eddy currents are induced. Carbon fibre has limited anisotropic conductivity, but inspecting it by ECT is a specialised application, not routine practice.
Does eddy current testing work through paint?
Through thin non-conductive coatings, yes — but coating thickness increases lift-off, which reduces sensitivity and must be accounted for in calibration. Heavy coatings degrade the inspection to the point of no value.
How deep can eddy current testing detect?
Depth depends on frequency, conductivity and permeability. In non-ferrous material, several millimetres at low frequency. In ferromagnetic steel, effectively surface only.
What is the difference between ECT and RFT?
Conventional ECT is limited by skin depth, which is very small in ferromagnetic material. RFT uses a through-transmission arrangement that overcomes this, making it the method for ferromagnetic tubing.
Do you offer eddy current testing?
No. This article is reference material. For the applications ECT commonly covers we provide ultrasonic and phased array testing, magnetic particle testing, penetrant testing, corrosion mapping and PMI — the table above indicates which fits each case.